WCSIPL delivers specialized HVAC solutions for sauces, gravies, and paste manufacturing facilities — maintaining the precise temperature and humidity conditions essential for product consistency, safety, and shelf life.
Viscous food processing — including sauces, gravies, pastes, and condiments — involves cooking, mixing, and packaging operations that generate significant heat, steam, and volatile organic compounds. Without specialized HVAC, these factors rapidly degrade product quality and plant hygiene.
WCSIPL designs and installs purpose-built climate control systems that address the unique environmental challenges of viscous food production, ensuring regulatory compliance and operational efficiency at every stage.
Standard commercial HVAC cannot handle the extreme heat, moisture, and contamination risks generated during viscous food processing operations.
Cooking kettles and jacketed vessels generate intense heat that raises ambient temperatures beyond safe operating limits, affecting both product viscosity consistency and worker safety in processing areas.
Boiling, simmering, and steam-based cooking release large volumes of moisture into the air. Uncontrolled humidity causes condensation on ceilings, equipment, and packaging — leading to microbial growth and product contamination.
Cooking aromas, spice particles, and airborne grease from multiple product lines create cross-contamination risks. Zoned HVAC with pressure cascades and filtration prevents flavor transfer and foreign particle ingress.
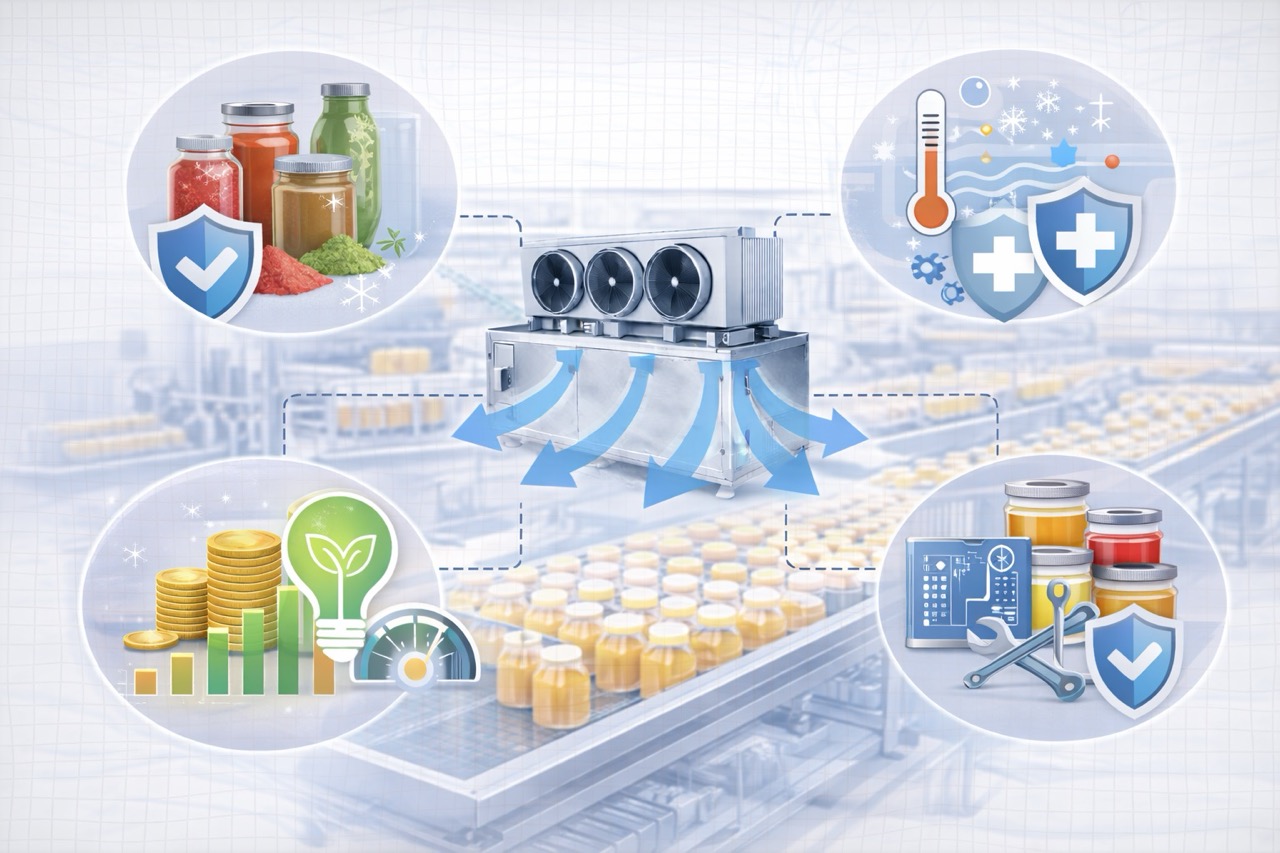
Purpose-engineered HVAC systems deliver measurable improvements in packaging quality, product safety, and energy performance.
Controlled temperature and humidity in filling zones prevents condensation inside jars, bottles, and pouches — ensuring seal integrity and label adhesion for viscous products.
Precise environmental control during hot-filling and cooling stages minimizes post-process contamination risk, directly extending product shelf life and reducing batch rejections.
Stable ambient conditions maintain consistent product viscosity, color, and texture across batches — preventing temperature-driven variations that affect thickening agents and emulsions.
Heat recovery from cooking exhaust pre-heats make-up air, while VFD-driven fans and intelligent controls reduce energy consumption by up to 30% compared to conventional systems.
Each system component is specifically engineered to handle the heat, moisture, and contamination challenges of sauces, gravies, and paste production.
High-capacity dehumidification systems maintain relative humidity between 40–55% RH in cooking and packaging zones, rapidly extracting moisture from boiling and simmering operations to prevent condensation and microbial growth on surfaces and equipment.
Multi-stage filtration with pre-filters, HEPA, and activated carbon beds removes spice particles, grease aerosols, and cooking odours from exhaust air — preventing cross-contamination between product lines and ensuring compliant discharge to atmosphere.
Zone-specific temperature control maintains ±1°C accuracy — from hot-cooking zones requiring high-volume heat extraction to cooling tunnels needing precise 20–25°C conditions for hot-fill product stabilization before capping and labelling.
All ductwork, air handling units, and exhaust hoods feature food-grade stainless steel construction with smooth welds, sloped drain pans, clean-in-place capability, and accessible inspection panels to meet FSSAI and HACCP hygiene requirements.
Our HVAC systems serve every critical zone in a sauces, gravies, and paste manufacturing facility — from raw material intake through to finished goods warehousing.

We bring deep domain expertise in food processing HVAC with a proven track record across India's leading sauce, gravy, and paste manufacturers.
Every HVAC system is custom-engineered based on your specific cooking processes, product types, and facility layout — not generic templates.
Systems designed to meet FSSAI, HACCP, BRC, and ISO 22000 requirements with complete documentation and validation support for smooth audits.
From design and engineering to procurement, installation, commissioning, and after-sales AMC — a single point of accountability for your entire HVAC project.
Heat recovery systems, VFD controls, and smart BMS integration reduce operational energy costs by up to 30% without compromising process conditions.
15+ years of specialized experience in food processing HVAC with 50+ successful installations across sauces, gravies, pastes, and condiment facilities.
Dedicated service teams with 24/7 breakdown support, preventive maintenance programs, and spare parts availability to ensure uninterrupted production.